


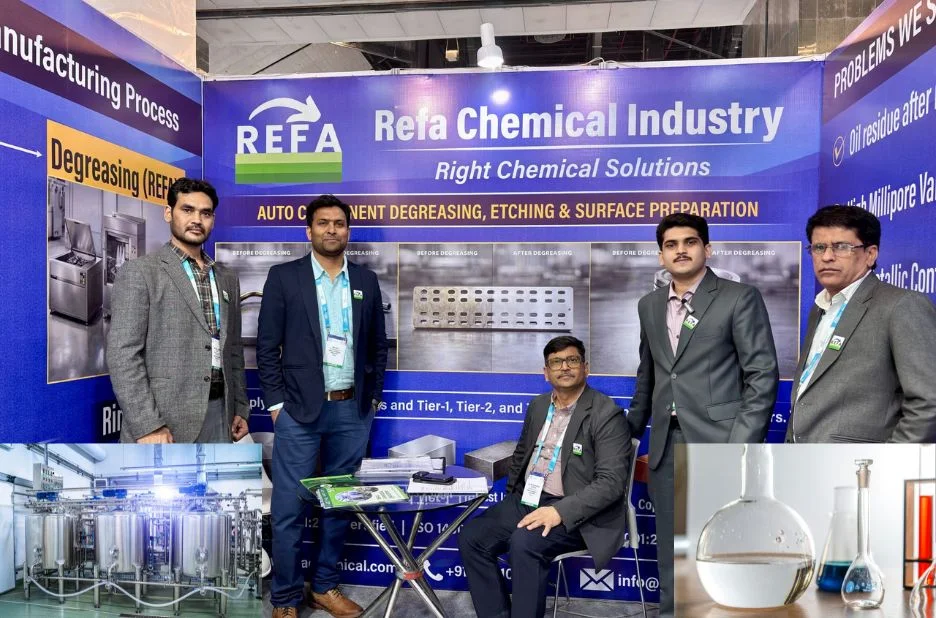
Innovations in Industrial Cleaning Technologies
In the realm of industrial cleaning, advancements in chemical formulations have significantly enhanced efficiency and environmental safety. Companies have shifted towards using specialized chemicals that not only improve cleaning performance but also comply with strict environmental regulations. These Refa Chemical Industry innovations allow for deeper cleaning of machinery and components, reducing downtime and extending equipment lifespan. Incorporating cutting-edge technology in chemical production ensures that industries can maintain high standards without compromising operational safety.
Importance of Quality Assurance in Chemical Manufacturing
Quality assurance plays a crucial role in the manufacturing of industrial chemicals. Precise formulations and consistent product quality are essential to meet the rigorous demands of industrial applications. Chemical producers invest heavily in research and development to ensure their products deliver reliable results. The adoption of international quality standards and certifications adds credibility and trust for clients worldwide. This focus on quality guarantees that the chemicals perform effectively in various conditions without adverse effects on machinery or the environment.
Applications in Surface Treatment and Degreasing
Surface treatment and degreasing are vital processes in many industries, including automotive, aerospace, and electronics. Proper cleaning agents remove contaminants such as oils, greases, and residues that can affect surface integrity and bonding. Advanced chemical solutions facilitate these processes by breaking down stubborn impurities while protecting the base materials. This ensures better adhesion for coatings, paints, or adhesives, ultimately improving product quality and durability. The development of specialized formulations tailored to different substrates has revolutionized surface preparation techniques.
Meeting Industrial Performance and Safety Standards
Adhering to industrial performance and safety standards is imperative for companies supplying chemicals for cleaning applications. Manufacturers must ensure their products are safe to handle, store, and use without causing harm to workers or equipment. This requires comprehensive testing, proper labeling, and adherence to regulatory guidelines. Chemicals that meet these standards contribute to safer work environments and reduce the risk of accidents. Additionally, high-performance chemicals increase operational efficiency by delivering consistent results under varying industrial conditions.
Conclusion
Industrial cleaning solutions are advanced with Refa Chemical Industry delivering ISO-certified chemicals for degreasing, surface treatment, and precision cleaning applications. refachemical.com provides reliable manufacturing quality for industrial performance and safety standards worldwide. Businesses seeking dependable chemical suppliers can benefit from the expertise and innovation offered by Refa Chemical Industry, ensuring their cleaning processes meet the highest expectations.